Industrial Valve Suppliers in Pune
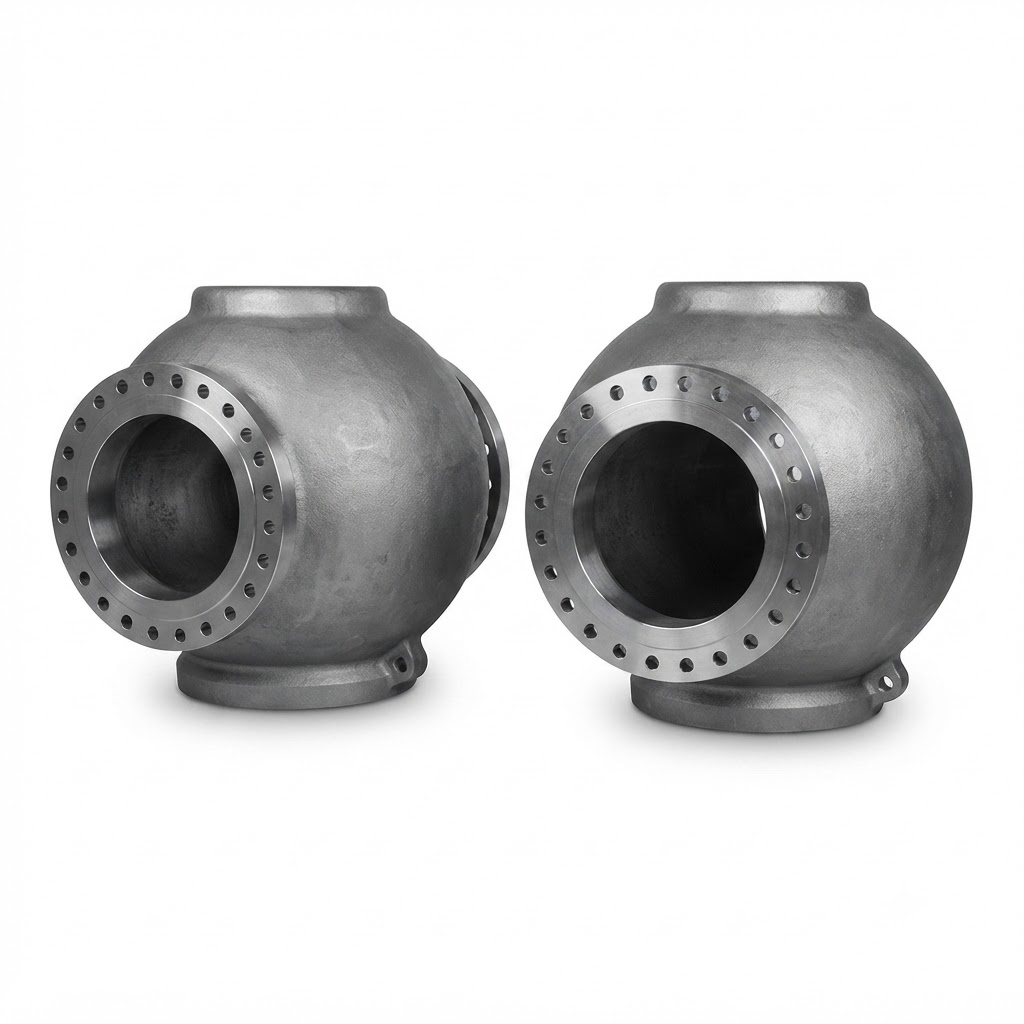
Aditya Metallic and Pipes is trusted Industrial Valve Suppliers and Dealers in Pune. We provide high-quality Industrial Valve solutions designed to support reliable and efficient operations across various industries.
With over 20 years of industry experience, advanced manufacturing expertise, and a strong focus on durability, we deliver valves that ensure precise flow regulation, safe process management, and long service performance. Our industrial valves are engineered using quality materials and modern production techniques to meet diverse industrial requirements.
We serve industries including oil, chemical, power, water, and manufacturing sectors with dependable products that enhance operational efficiency. We continuously focus on quality, innovation, and customer satisfaction to deliver trusted valve solutions for industrial applications.
What Is an Industrial Valve and How Does It Support Efficient Flow Control?
An Industrial Valve is an essential flow control device used to start, stop, regulate, or redirect the movement of fluids and gases within industrial systems. These valves play a vital role in maintaining safety, efficiency, and performance in industries such as manufacturing, energy, and processing. The Importance of Valves in Industrial Processes is significant because they ensure smooth operation of Industrial piping systems and reliable fluid management.
Working Principle of Industrial Valve
We design and supply industrial valves that ensure efficient fluid control by regulating flow, pressure, and process operations with reliable performance across demanding industrial environments.
- Controls Fluid Flow: Industrial valves regulate, start, stop, or redirect the flow of liquids, gases, steam, and other process media in piping systems.
- Operates Through a Control Element: Valves use components like gates, balls, discs, plugs, or diaphragms to manage the flow path.
- Open Position: When opened, the internal element moves away from the passage to allow smooth fluid movement.
- Flow Regulation Position: Partial opening helps control flow rate, pressure, and fluid volume as required.
- Closed Position: The sealing element blocks the flow path completely to prevent leakage and stop fluid movement.
- Manual or Automated Operation: Valves can be operated manually or through pneumatic, electric, and hydraulic actuators.
- Pressure Control: Industrial valves maintain required pressure and flow levels for efficient process operations.
- Leak Prevention: High-quality sealing systems minimize leakage and improve safety and reliability.
- Handles Harsh Conditions: Industrial valves are designed to withstand high pressure, extreme temperatures, and corrosive environments.
- Supports Process Efficiency: Accurate flow control helps improve safety, productivity, and overall system performance.
Types of Industrial Valve
As Industrial Valve Suppliers in Pune, we offer a wide range of industrial valves engineered for isolation, flow regulation, safety, and process control applications across various industries.
- Isolation and Shutoff Valves:
- Gate Valves: They use a lifting wedge or gate mechanism to completely open or close the pipeline flow path. These valves are ideal for full isolation applications where minimum flow resistance is required.
- Ball Valves: They use a rotating ball with a bore to provide quick quarter-turn operation and tight sealing. These valves are suitable for applications requiring fast shutoff and reliable flow control.
- Butterfly Valves: They feature a rotating disc inside the pipeline to regulate or isolate fluid movement. These valves offer a compact, lightweight, and cost-effective solution for large piping systems.
- Plug Valves: They use a tapered or cylindrical plug to control, stop, or redirect fluid flow. These valves are widely used in demanding applications such as oil, gas, and industrial processing systems.
- Flow Control and Regulation Valves:
- Globe Valves: They are designed with a plug and seat arrangement to provide accurate flow adjustment. These valves are commonly used where precise throttling and flow regulation are required.
- Needle Valves: They use a fine pointed plunger to achieve precise control of low-volume liquid and gas flow. These valves are suitable for instrumentation and applications requiring accurate metering.
- Diaphragm Valves: They operate using a flexible membrane that separates process fluids from internal components. These valves are preferred for corrosive, hygienic, and sensitive fluid handling applications.
- Pinch Valves: They control fluid movement by compressing a flexible sleeve within the valve body. These valves are effective for handling slurries, powders, and media containing solid particles.
- Safety and Non-Return Valves:
- Check Valves: They allow fluid flow in only one direction and automatically prevent reverse movement. These valves help protect pumps, pipelines, and equipment from backflow-related damage.
- Safety / Relief Valves: They automatically release excess pressure when system limits are exceeded. These valves protect industrial equipment and improve safety in high-pressure applications.
Components of Industrial Valve
As Industrial Valve Dealers in Pune, we provide valves built with precisely engineered components that ensure durability, accurate operation, and long-term reliability in industrial systems.
| Component | Description |
|---|---|
| Body | It is the main outer shell that holds the fluid passage and connects the valve with piping systems. |
| Bonnet | It is the top cover that protects internal parts and provides proper sealing with the valve body. |
| Disc (Obturator) | It is the moving element, such as a wedge, ball, or plug, that controls fluid flow. |
| Seat | It is the sealing surface where the disc rests to prevent leakage when the valve is closed. |
| Stem | It connects the external operating mechanism with the internal disc to control valve movement. |
| Packing | It is a sealing material around the stem that prevents external fluid leakage. |
| Actuator | It is the operating mechanism that opens or closes the valve using manual, electric, pneumatic, or hydraulic power. |
Key Features of Industrial Valve
As Industrial Valve Suppliers in Pune, we deliver high-performance valves equipped with advanced materials, superior sealing, and automation-ready features to meet modern industrial requirements.
- High-Quality Material Construction: Our Industrial Valve materials and construction ensure excellent strength, durability, and resistance against demanding industrial operating conditions.
- Precision Flow Control: These valves provide accurate regulation of liquids, gases, and steam, making them an essential part of efficient Flow control equipment.
- High Pressure Performance: Designed for challenging applications, these valves offer reliable operation with excellent Industrial valve pressure rating capabilities.
- Advanced Sealing Technology: Equipped with reliable sealing systems, these valves minimize leakage and improve safety across various industrial processes.
- Automation Compatibility: These valves support modern Industrial valve automation with pneumatic, electric, and other advanced actuation systems for efficient process control.
Benefits of Industrial Valve
As Industrial Valve Dealers in Pune, we provide reliable valve solutions that enhance safety, improve efficiency, reduce maintenance needs, and support smooth industrial operations.
- Improved Operational Safety: Industrial valves help maintain controlled flow conditions, protect equipment, and enhance safety in critical industrial operations.
- Enhanced System Efficiency: They improve the performance of Industrial fluid handling systems by providing smooth and reliable flow management.
- Long Service Life: Durable construction and corrosion-resistant industrial valves technology help reduce maintenance needs and increase operational lifespan.
- Reduced Downtime and Maintenance Costs: Reliable valve performance minimizes unexpected failures and supports efficient Industrial valve maintenance practices.
- Better Process Control: These valves ensure accurate fluid regulation and support efficient Process control systems across multiple industries.
Applications of Industrial Valve
As Industrial Valve Suppliers in Pune, we supply versatile valve solutions designed to support critical fluid handling and process control requirements across multiple industrial sectors.
- Oil and Gas Industry: Industrial valves are widely used in pipelines, refineries, and processing units for safe flow control and pressure management in the Oil and Gas Industry.
- Water and Wastewater Treatment: These valves support water distribution, filtration, and treatment operations in water treatment plants for efficient fluid handling.
- Power Generation Plants: Industrial valves help control steam, cooling water, and other process fluids to maintain reliable operations in power generation facilities.
- Chemical Processing Industry: These valves provide safe and precise control of chemicals in chemical factories where corrosion resistance and durability are essential.
- Petrochemical Industry: Industrial valves are used in petrochemical processes for handling high-pressure fluids and maintaining safe pipeline operations.
- Pharmaceutical Manufacturing: These valves support hygienic fluid transfer and precise process control requirements in pharmaceutical production environments.
- Food and Beverage Processing: Industrial valves ensure clean and controlled flow management for maintaining quality and safety in food processing applications.
- Mining and Mineral Processing: These valves are used for slurry handling and heavy-duty applications where reliable performance under harsh conditions is required.
Why Choose Us?
- 20+ Years of Industry Expertise: We bring over two decades of manufacturing experience to deliver reliable Industrial Valve solutions with proven quality, technical knowledge, and industry-focused performance.
- Quality-Driven Manufacturing Approach: We focus on advanced production methods, premium materials, and strict quality checks to provide durable valves that meet diverse industrial requirements.
- Customer-Focused Valve Solutions: We provide customized support, reliable products, and efficient service to help industries achieve safe, smooth, and cost-effective flow management.
Choose Aditya Metallic and Pipes is prominent Industrial Valve Suppliers and Dealers in Pune. We deliver dependable Industrial Valve solutions designed for performance, durability, and efficient flow control. With years of expertise, quality manufacturing, and customer-focused services, we support industries with reliable valve products that improve safety, productivity, and long-term operational efficiency. Reach out to us for more information.
FAQ’s
Industrial valves are flow control devices used to start, stop, regulate, and redirect liquids, gases, and other process media in industrial systems. They are important for ensuring safe operations, efficient flow management, and reliable process performance.
An industrial valve controls the movement of fluids within pipelines by adjusting, isolating, or directing flow. It helps maintain system safety, pressure control, and operational efficiency.
An industrial valve works by moving an internal component such as a disc, ball, gate, or plug to control fluid passage. The operation can be manual or automated depending on the application.
Manual valves are operated using handles, wheels, or levers, while automated valves use electric, pneumatic, or hydraulic actuators. Automated solutions improve efficiency in advanced process control systems.